Uniaxial Geogrid Exporter Checklist for Successful Road Projects
2026-10-09
Every road project begins with a promise: that the ground beneath will hold. For engineers and contractors who stake their reputation on uniaxial geogrid performance, the difference between a smooth opening and a costly failure often comes down to one thing—choosing the right exporter. That’s where a practical checklist saves more than time; it saves the road itself. From raw material integrity to roll-width tolerance and load-test documentation, the details are unglamorous but unforgiving. Over the years, WEN FENG STONE has seen how a single overlooked spec can ripple into subgrade settlement or pavement cracking months after the ribbon cutting. So before you sign off on your next shipment, ask yourself: does your supplier’s checklist match the reality of your job site? In the following sections, we’ll walk through the non-negotiables that separate a dependable geogrid partner from a gamble.
Inspect Roll Core Alignment Before Container Stuffing
Before any rolls go into the container, a visual check of core alignment takes only a minute but catches most failures. Look straight through each core and compare its position to the roll face on both sides. If the core sits high on one side or has started to telescope, the load will never brace evenly.
Line up several rolls with their open ends facing the same direction. Run a straightedge or a laser across the core ends. Any core more than a few millimeters out of line means that roll should be pulled aside and rechecked. A core that is cocked inside the roll body is worse than one that is simply offset, because it changes how the roll’s weight transfers through the cradle or chock.
Once the cores are aligned, press on each core plug to confirm it is fully seated. Re-tension or replace straps if the plug shifts, and reject any roll with a crushed or oval core end. The goal is to load only rolls with straight, centered, fully supported cores—anything less tends to translate into torn wrapping, shifted cargo, and damaged edges before the container reaches the port.
Compare Geogrid Rib Tensile Strength to Project-Specific Design Loads
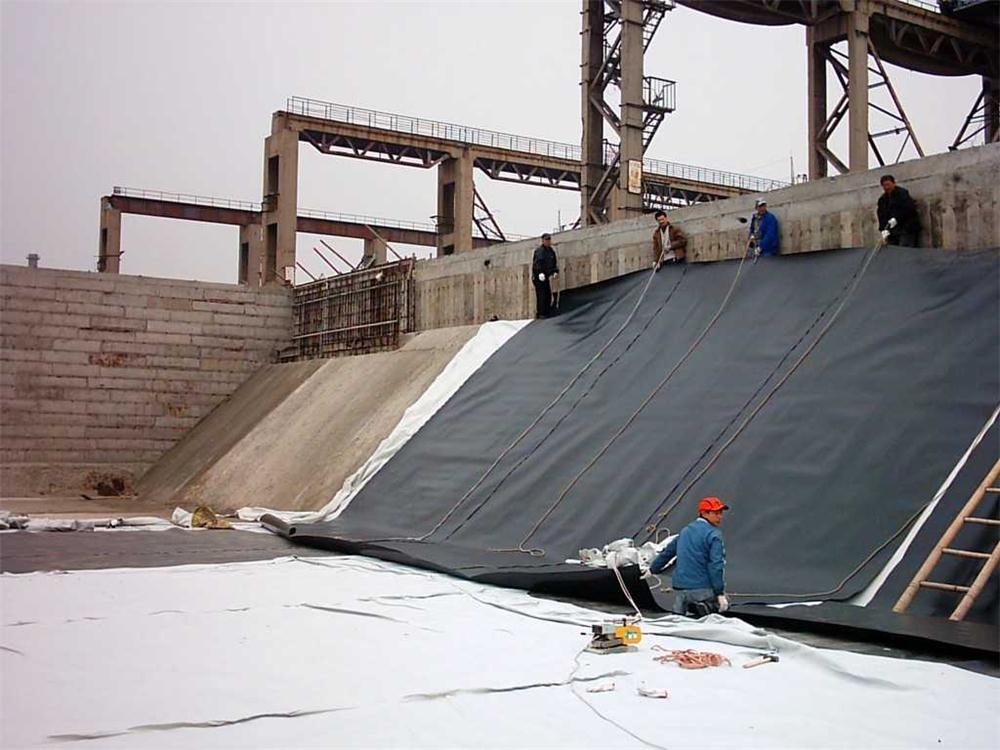
The tensile strength of a geogrid rib is not a single catalog number you can drop directly into a design. A wide-width tensile test gives an ultimate value under a specific strain rate and confinement, but the rib must still function after decades of creep, installation damage, and chemical exposure. Comparing that raw rib strength to project design loads without adjusting for these time-dependent and site-specific factors almost always overestimates real performance.
Start by reducing the short-term rib strength using the standard partial factors for creep, installation damage, weathering, and joints or connections. That gives you the long-term design strength per rib or per unit width. Then pull the governing tensile demand from your slope stability, pavement, or retaining wall analysis. If the demand comes from a finite element or limit equilibrium output, convert it to force per rib at the spacing you intend to use, not just an average stress across the fabric.
The comparison should also account for how load actually enters the ribs. Junction efficiency and the transverse rib contribution can shift stress concentrations, so the peak rib tension may be higher than an evenly distributed estimate. Where the allowable rib strength falls short of the demand, increasing rib cross-section or reducing spacing helps, but only after checking that the failure mode hasn’t shifted to pullout or connection slip.
Request Accelerated Weathering Data for Coastal Geogrid Exposures
The corrosive bite of salt spray, relentless UV radiation, and temperature swings in coastal zones often undermine the long-term performance of geogrids used in reinforced slopes and retaining walls. Requesting accelerated weathering data before specifying a product can reveal how its polymer structure holds up under simulated marine conditions—think xenon-arc chambers that condense years of sun and salt fog into a few weeks. Look for reports that go beyond tensile strength retention and include changes in aperture stability, junction integrity, and surface oxidation, since these factors directly influence load transfer and drainage in coastal fills.
Not all accelerated weathering protocols are equal, so the request should specify exposure parameters that match the project site. For instance, a geogrid buried behind a seawall may face less direct UV but higher chloride ingress than one exposed during construction staging. Ask for data generated under cyclic salt spray plus UV-A or UV-B cycles, with temperature ramping that mirrors tidal fluctuations. Reputable suppliers will share time-to-embrittlement curves, molecular weight loss rates, and visual crack propagation maps alongside standard ISO or ASTM test references.
When evaluating the returned data, avoid treating a single pass/fail number as the whole story. Coastal projects often require a safety margin that accounts for microcracking from wind-blown sand abrasion and alkaline concrete contact. Cross-check the accelerated weathering results against any available natural exposure data from similar latitudes, and request a written interpretation from the manufacturer's polymer engineer. A thoughtful data package lets you compare candidate geogrids not just by initial cost, but by the replacement cycles avoided over a 75-year coastal service life.
Mark Every Geogrid Roll with Batch-Linked Traceability Codes
Assigning batch-linked traceability codes to every geogrid roll turns a routine labeling step into a reliable production fingerprint. Raw polymer lot numbers, extrusion line settings, and final roll identifiers all sit behind a single code, so each roll can be traced back to its exact manufacturing window without digging through paper logs.
On site, this matters most when a shipment contains multiple lots or when rolls look identical after wrapping. A quick scan lets the crew confirm that the right product is going into the right reinforcement layer. It also prevents older stock from being used accidentally ahead of newer rolls, which keeps project documentation cleaner.
If a problem appears later, the code narrows the investigation fast. Engineers can pull the exact quality-control records for the rolls installed in a specific area, compare them against lab test data, and isolate a suspect batch without stopping work across the whole site. That level of granularity turns traceability from a paperwork requirement into a practical field tool.
Supply Bilingual Geogrid Installation Sequence Cards for Field Crews
We keep a stack of laminated sequence cards in the site trailer, each one printed with Spanish on one side and English on the other. The steps follow our actual roll-out pattern for geogrid: stake the leading edge, pull the roll taut, notch around drainage structures, then overlap at the painted line. No one has to wonder whether “tension” means the same thing twice, because the drawing and the verb line up on both sides of the card.
Crew leads hand these out during tailgate talks and after close calls, not just at orientation. That way the sequence gets absorbed in small doses instead of getting buried in a manual. We also keep a weatherproof set in the cab of the sheepsfoot roller so the cards survive rain, mud, and diesel-soaked gloves. When a new operator starts mid-shift, the card gives them the exact overlap and pinning order before they have to flag down the foreman.
For the night shift, the cards are printed with high-contrast icons and oversized text so they stay readable under tower lights or a headlamp. The side-by-side wording also lets a bilingual crew member walk someone through a step in either language without pulling the whole laydown crew off the line.
Validate Geogrid Junction Efficiency Using Site-Sampled Backfill
Geogrid pullout capacity in reinforced soil relies heavily on how efficiently load transfers at the rib intersections. A junction that fails prematurely lets transverse ribs rotate or displace without developing the full bearing resistance of the surrounding backfill. When site-sampled material is used instead of a manufactured sand or gravel, the confinement, particle interlock, and compaction behavior around those junctions reflect the actual soil that will surround the reinforcement in the finished structure.
Validation testing typically starts with collecting several representative samples from the borrow source or stockpile that will supply the reinforced fill. The soil is characterized for gradation, Proctor moisture-density relationship, and direct shear strength, then recompacted to the target field density and moisture in a large pullout box. The geogrid is embedded in that soil and pulled horizontally while the junction strength is measured under confinement. The resulting junction efficiency, calculated as the sustained junction load divided by the rib ultimate tensile strength, is then checked against the value used in design calculations.
Site soils often contain a wider range of particle sizes, angular chips, or fine-grained material than typical laboratory test fills. These differences can work in both directions: crushed angular backfill may wedge tightly into the geogrid apertures and improve junction confinement, while excessive fines or rounded particles can reduce interlock and allow junction slip at lower loads. Testing with the actual backfill removes that guesswork and gives a measured basis for adjusting anchorage lengths or accepting a geogrid product, rather than relying on generic pullout coefficients.
FAQ
The melt flow index and carbon black dispersion need to fall within a tight range, because road-grade geogrids live under asphalt for decades. A batch with poor UV stabilizers will surface as premature cracking long before the project warranty ends.
Junction efficiency tells how well ribs transfer load at intersections. If the junctions are weak, the grid behaves like loose strips instead of a continuous plane, and aggregate interlock under trafficking loads fails progressively.
Request the exact width, length, and core diameter for each order. Road projects often design around standard paving widths, so a roll that arrives 20 centimeters too wide can force manual cutting and slow down the paving crew.
Include a certified mill test report, third-party tensile test results, roll traceability labels, and a signed compliance statement matching the project specification. Missing paperwork often stops material at the gate even when the product is fine.
Use UV-stabilized wrapping, stack rolls on edge rather than flat, and block them with wooden chocks inside the container. Edge protectors on the roll ends also stop impact tears when the container is shifted at port.
Check ribs for uniform thickness, measure aperture dimensions in several roll locations, and sample-test tensile strength at both room temperature and elevated temperature. Photograph the loaded rolls and seal the container with a tamper-evident tag.
Carbon black absorbs UV radiation and slows oxidation in polyethylene. Road geogrids get exposed to sunlight during staging and installation, so low carbon black content can lead to surface embrittlement before the base course is placed.
Confirm whether the road requires primary reinforcement along the traffic direction or transverse to it. Uniaxial geogrids are optimized for one main load axis, so matching the rolled orientation to the design direction avoids wasted strength and uneven deformation.
Conclusion
Before any uniaxial geogrid leaves the factory, a handful of practical checks make the difference between a smooth road project and a costly rework. Start by confirming roll core alignment before container stuffing; a shifted core can crush ribs during transit and create hidden weak points that only show up on site. Then compare the geogrid's rib tensile strength against the project-specific design loads, not just the generic product datasheet. Coastal exposures add another layer: request accelerated weathering data so you know the polymer won't lose too much strength under salt spray and UV. These early verifications may seem like paperwork, but they prevent a geogrid from arriving with damage, underperformance, or premature aging already baked in.
Once the material reaches the worksite, traceability and installation clarity take over. Mark every roll with batch-linked traceability codes so any quality question can be traced back to raw material and production records within minutes. For field crews who speak different languages, supply bilingual installation sequence cards rather than relying on verbal instructions; a simple visual step-by-step card reduces orientation errors and speeds up laying. Finally, validate geogrid junction efficiency using site-sampled backfill—laboratory numbers don't always match real soil friction and interlock. Pulling a few junction tests with the actual backfill gives the exporter and contractor confidence that the reinforcement will hold the design load without excessive deformation. These steps turn a standard export checklist into a practical guardrail for successful road projects.
Contact Us
Contact Person: Jennifer LEE
Email: [email protected]
Tel/WhatsApp: 8618553418999
Website: https://vip.e-baixing.com/wenfengshitong