Best Ductile Iron Casting Methods for Stronger Metal Parts
2026-09-16
If you've ever machined a ductile iron part that chipped too easily or failed under load, you know the casting method is not a minor detail. At Zhaoyuqi, we've seen first-hand how choosing the right process—whether it's shell molding, lost foam, or resin sand—can double the strength of the final metal part. This post breaks down the best ductile iron casting methods that consistently produce stronger, more reliable components, along with the trade-offs you need to know before placing your next order.
Sand Casting's Continued Edge for Heavy-Duty Ductile Iron Parts
Sand casting remains the backbone for producing large ductile iron components where strength and fatigue resistance are non-negotiable. Unlike die casting or permanent mold processes, sand molds accommodate the slower cooling rates that heavy sections demand, preventing carbide formation and preserving the graphite nodule structure that gives ductile iron its toughness. This is especially critical in castings weighing several hundred pounds, where thermal gradients can easily compromise mechanical properties if not carefully managed.
The flexibility of sand casting also allows engineers to optimize gating and risering for each specific geometry, ensuring directional solidification without the geometric constraints of machined dies. For heavy-duty applications like axle housings, pump bodies, or gearbox casings, the ability to adjust mold materials, coatings, and pouring temperatures on a per-job basis delivers consistent results across low-to-medium production runs. Tooling costs stay reasonable compared to high-pressure die casting, and design changes can be implemented quickly by reworking patterns rather than replacing entire die sets.
Beyond process control, sand casting continues to deliver economic advantages for large ductile iron parts where the alternative would be fabrications or steel castings. Ductile iron’s yield strength paired with sand casting’s tolerance for thick walls and complex cores often eliminates the need for welded assemblies, reducing both manufacturing steps and potential failure points. With modern simulation software and no-bake sand systems, foundries now achieve dimensional accuracy and surface finish that rival other methods, making sand casting not just a legacy choice but a deliberate engineering decision for heavy-duty reliability.
The Simplification Lost Foam Brings to Complex Designs
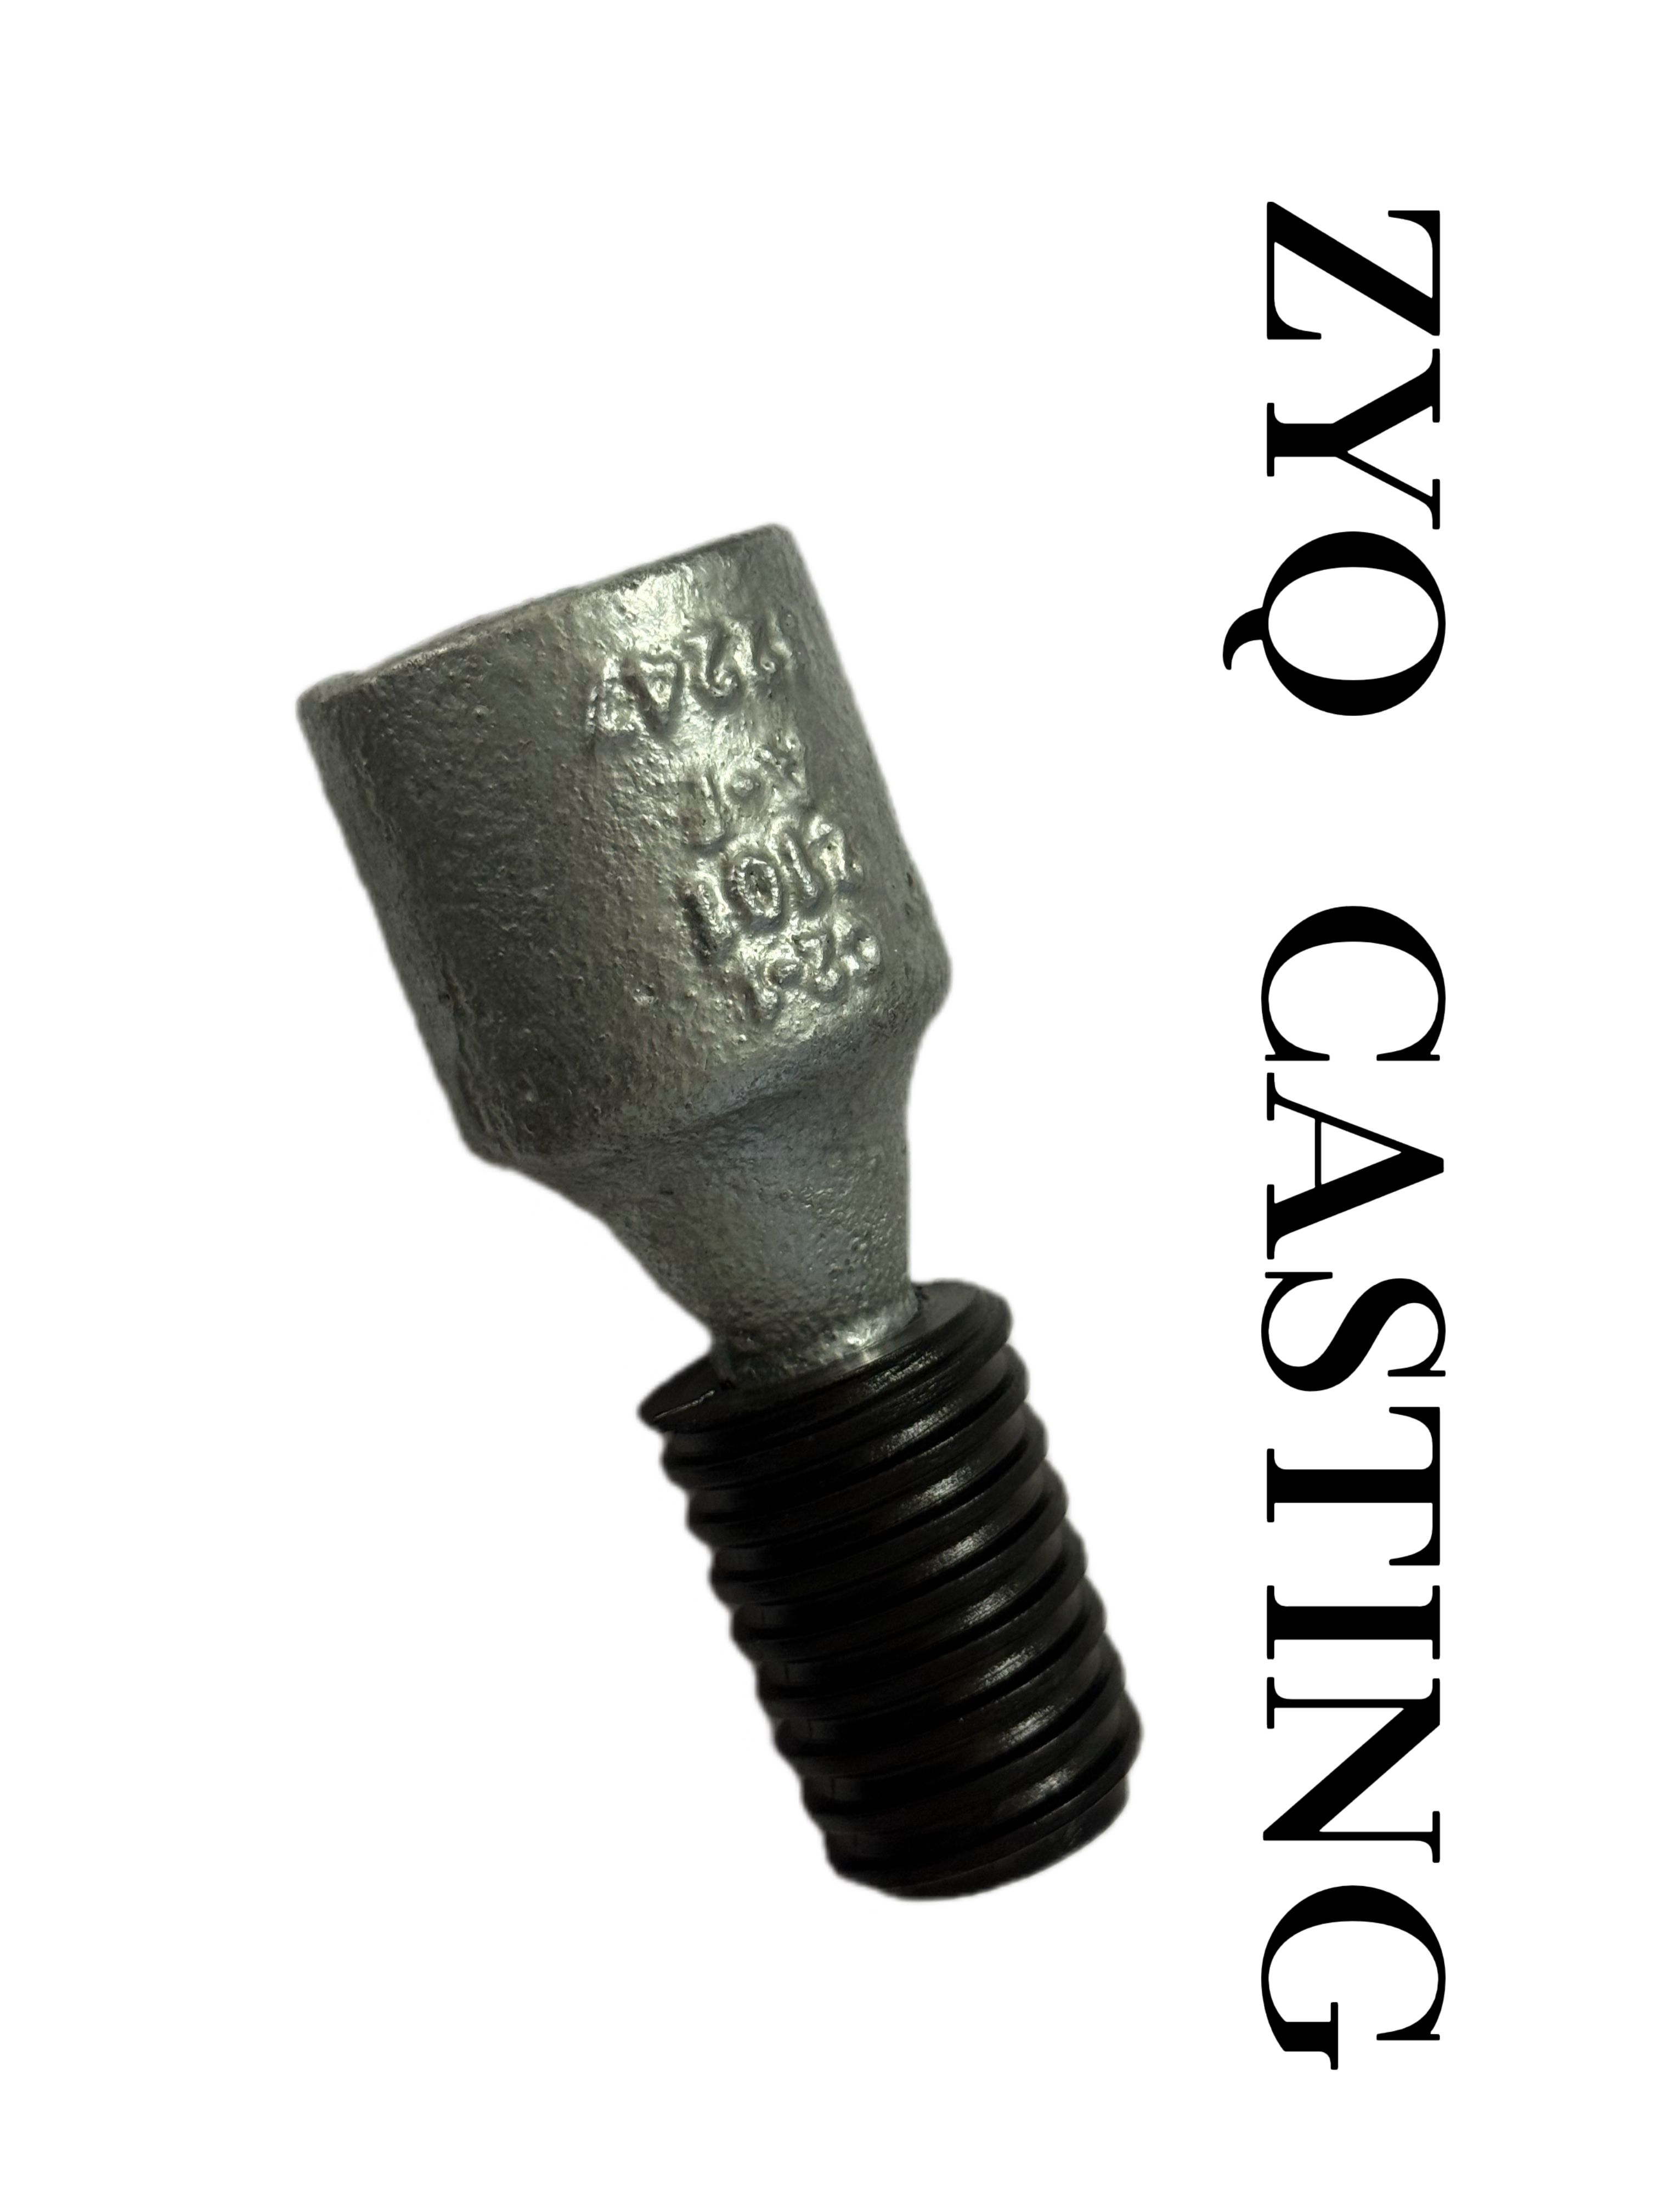
In conventional sand casting, achieving intricate internal cavities often means juggling multiple cores, each needing precise placement and support. Lost foam eliminates that entire choreography. The foam pattern stays embedded in the sand, and the molten metal simply takes its place, vaporizing the foam as it flows. There are no parting lines to constrain geometry, no cores to shift or break. A water jacket, an exhaust manifold with twisted passages, or a hydraulic manifold with intersecting channels can be produced in a single pour, exactly as designed, without the assembly headaches.
This freedom lets engineers consolidate what used to be assemblies of several cast or machined parts into one near-net-shape component. Brackets, flanges, and mounting bosses that were once bolted or welded on can now be cast integrally. The result is fewer joints, fewer potential leak paths, and a shorter bill of materials. It also cuts down on secondary machining because many functional surfaces, like internal threads or sealing faces, can be formed directly in the casting process. For complex designs, that's not just a convenience—it's a fundamental shift in how parts can be imagined.
Perhaps the most underappreciated simplification is in the design iteration loop. Changing a complex cast component in traditional tooling often means reworking steel molds or core boxes, which is expensive and slow. With lost foam, the pattern is typically machined from expanded polystyrene or copolymer beads, so a design change may only require a new foam pattern, not a whole new tooling suite. This accelerates prototyping and lets design teams test multiple configurations without committing to hard tooling upfront, making complexity less of a risk and more of an opportunity.
Centrifugal Casting as a Fix for Centerline Shrinkage
When a conventional static casting cools, the last metal to solidify often sits along the central axis of the part. Without a nearby riser or careful hot spot control, that zone can pull open into a string of voids known as centerline shrinkage. In bars, billets, and thick cylindrical sections, those internal cavities weaken the cross-section and only become obvious after machining or sectioning.
Centrifugal casting sidesteps the problem by rotating the mold while the metal freezes. The spin creates radial pressure that feeds liquid into areas where solidification is still happening. Instead of relying only on gravity-fed risers through a long narrow path, the entire inner surface acts as a feeding reservoir. Shrinkage that would normally collect in the center gets pushed to the bore, where it appears as a thin sacrificial layer that can be machined away. This is why the method works well for pipes, rings, and sleeve-type parts that need full wall thickness integrity.
There are practical limits, though. The inner surface still requires a cleanup pass, and mold speed has to stay high enough to maintain feeding pressure until the last liquid solidifies. For alloys with a wide freezing range, some microporosity can remain near the bore, but the centrifugal feed usually keeps it diffuse rather than allowing a continuous centerline defect to form.
Mechanical Uniformity Through Continuous Casting
Continuous casting replaces the stop-start rhythm of ingot pouring with a steady solidification front that moves through a water-cooled copper mold and secondary spray zones. Because the shell forms under nearly constant thermal gradients, the resulting billet or slab avoids the random chill crystals and abrupt columnar-to-equiaxed transitions that make conventionally cast metal behave differently from surface to center.
Pull speeds, mold oscillation, and secondary cooling are tuned so that the last liquid to freeze remains shallow and dispersed rather than pooling at the centerline. This directly reduces centerline segregation, porosity, and micro-shrinkage—three defects that routinely create weak bands in ingot-cast stock. Tensile strength, ductility, and hardness then stay within a much tighter band when test coupons are cut from edge, quarter, and core locations.
Further gains come from in-line techniques like electromagnetic stirring and soft reduction. Stirring shears the mushy zone and encourages a finer, more equiaxed grain structure; soft reduction closes the remaining liquid channels before they can form voids. The result is a cast product whose mechanical response is governed by composition and cooling history, not by which part of the cross-section happens to be sampled.
Shell Mold Casting for Fewer Secondary Operations
Shell mold casting stands out for producing parts that need far fewer finishing steps. The resin-coated sand shell is rigid and dimensionally stable, so the casting picks up fine details from the metal pattern with minimal shrinkage or distortion. As a result, the as-cast surface is much smoother than what you get from green sand or many other processes, often eliminating the need for extensive grinding or polishing before the part is ready.
Many features that would normally require separate machining can be formed directly in the mold. Internal cavities, bolt bosses, ribs, and even some small holes can be cored or shaped during casting, so drilling, milling, or tapping operations drop off the production sequence. This is especially useful for complex housings, valve bodies, and similar components where post-casting work is a major cost driver.
Because the metal pattern is reusable and the shell-making process is automated, dimension accuracy stays consistent from one part to the next. Tolerances are tight enough that reaming or corrective machining is often unnecessary, and the smooth parting lines reduce the need for hand finishing. Choosing shell mold casting for the right parts moves much of the work into the mold itself, cutting labor and lead time downstream.
Thin-Walled Ductile Iron Success with Investment Casting
Thin-walled ductile iron parts used to mean trouble: cold shuts, hard edges, and graphite degradation. Investment casting flips that. By managing shell preheat and using ceramic cores only where needed, foundries now pour sections as slim as 2 mm and still get fully nodular microstructures in the final casting. The result is a part that behaves like ductile iron but weighs like an aluminum design.
The real lever is gating. Thin walls freeze fast, so the mold needs short, direct runners and carefully placed risers. When that is done right, you can hold flatness within 0.005 inch per inch and avoid the machining stock that used to erase the weight savings. As-cast tensile values above 65 ksi and elongation near 12% are regularly reported for these components, making them viable for brackets, sensor housings, and electric motor end bells.
One project replaced a multi-piece steel fabrication with a single investment-cast ductile iron bracket at 40% lower piece cost. The casting weighed 2.3 pounds, had 3 mm walls, and required only drilling and tapping. That kind of outcome is why more design teams are treating thin-wall ductile iron as a legitimate option instead of a last resort.
FAQ
Ductile iron contains spheroidal graphite instead of flakes, so stress concentrations are much lower, giving it higher tensile strength, elongation, and impact resistance. This makes it more suitable for parts that experience cyclic loading or sudden shocks.
Shell mold casting tends to provide tighter dimensional control than green sand because the resin-bonded sand mold is stiffer and smoother. For small to medium parts where precision matters, shell molding is often preferred over traditional sand casting.
Lost foam casting uses a foam pattern that vaporizes when metal is poured, leaving a single-piece mold without parting lines or cores. This reduces turbulence and misalignment defects, resulting in more uniform mechanical properties from part to part.
Centrifugal casting works well for symmetrical shapes like pipes, cylinder liners, and bushings. The spinning forces impurities and gas toward the inner surface, which can be machined away, leaving a dense, strong metal wall with fine grain structure.
Yes, austempering is a common heat treatment that transforms ductile iron into austempered ductile iron (ADI). ADI can reach tensile strengths over 1000 MPa while retaining good ductility, making it competitive with some steels for gears and shafts.
Nodularity refers to the percentage of graphite that forms as spheres rather than flakes. Higher nodularity generally means better elongation and fatigue strength. Foundries control this through magnesium treatment and inoculation, aiming for at least 80-90% nodularity in critical parts.
Resin sand molds have higher strength and better surface finish than green sand, so they can support larger, heavier castings without mold wall movement. This helps maintain dimensional accuracy and reduces the risk of shrinkage defects in thick sections.
Common defects include shrinkage porosity, dross inclusions, and carbides. Shrinkage can be controlled with proper gating and risering; dross is minimized by using filters and clean metal handling; carbides are avoided by balanced inoculation and avoiding excessive cooling rates.
Conclusion
When manufacturers need ductile iron components that hold up under heavy loads, sand casting still earns its place. The process works well for large, thick-walled parts because the mold can be shaped to handle thermal stress and varied section sizes without driving up cost or complexity. Lost foam casting steps in when a design includes hidden channels or irregular contours. By placing a foam pattern directly in the sand and letting the molten metal burn it away, the method removes the need for multiple cores and reduces the chance of misalignment. This simplification often shortens lead times and opens up geometries that would be difficult to achieve with traditional molding. Both approaches highlight how choosing the right casting route depends on part size, internal complexity, and the level of strength required in service.
For parts that must resist internal defects, centrifugal casting forces metal outward as the mold spins, which helps eliminate centerline shrinkage and produces a dense, uniform structure in cylindrical components like pipes and bushings. Continuous casting offers another path to consistency by drawing material through a water-cooled die, creating long bars or tubes with stable mechanical properties from one end to the other. Shell mold casting uses a resin-bonded sand shell to deliver tighter dimensional control and smoother surfaces, cutting down on grinding or machining after casting. When ductile iron parts have very thin walls, investment casting becomes the better option, since the ceramic shell holds fine detail and yields a clean finish that often needs little rework. Each method brings a distinct advantage, so the strongest result comes from matching the technique to the shape, volume, and performance demands of the component.
Contact Us
Contact Person: Nico Yin
Email: [email protected]
Tel/WhatsApp: 8618561567088
Website: https://www.ductileironparts.com/